
Rigidity of GAP elements in contact
GAP element rigidity will depend on the material of the parts in contact... and also on the mesh size! Learn how to calculate it!
12 December 2022We were recently hired to investigate the cause of pressure vessel failure. In my line of work, I can rarely post pictures or outcomes of analysis that we do “commercially”. This time it’s different, so I just couldn’t miss the opportunity! Especially since this will be a great educational case-study!
In this article, we will analyze a failure of a pressure vessel. We will search for the cause of failure, and wonder what to do to avoid such issues in your design. And all of that using Engineering Judgment and Nonlinear FEA.
As you can imagine, there will be no names, locations and many “sensitive details”. After all, this is a delicate topic, that is still fresh as I’m writing this. However, I got the permission to use pictures as well as description of the failure (and our outcomes)!
This means that I can write a real industry-grade case study – how awesome is that!
The analyzed vessel belonged to a new installation. As with all of such systems, the vessel passed all the leaking tests and pressure tests. Of course, the tests showed no warnings. After all the tests, operator planned the first run.
There were 4 vessels that could be in operation in the installation. For the first run, the operator decided to use only one of those (the smallest vessel of the 4).
After the “first run” started, technical crew noticed a leak from one of the bigger vessels. Of course, they reasonably stopped the process.

Initially the assumption was that this is a minor issue with a weld or something similar. However, after the technical crew inspected the inside of the 2 bigger vessels they saw this:

At this point, as you can imagine things became way more serious. It became apparent that it’s definitely NOT a “small thing”.
As usually in such cases, at some point operator sent a claim to an insurance company they worked with. And that insurer hired an “external expert” (yours truly) to establish the reason of the failure.
I received a set of photographs of what happened (I showed you the most important ones above, of course there were many more). Additionally I received a surprisingly vague drawing documentations of the vessels.
Sidenote:
It’s “funny” how difficult it is to obtain the complete drawing documentation of the vessel when something “goes wrong”.
… not to even mention calculations of any kind, that were performed.
Anyway, based on the drawings I had, I managed to establish that the vessels looked more or less like this:

If you like the challenge:
At this point, I already knew what caused the failure.
During works, more details became available (thicknesses were measured on site, some extra details became “confirmed” etc.).
But the reality is, that what you know already is enough to realize what caused the failure!
If you wish, try to check the failure source from the info above*
*Definitely let me know in the comments how you did!
Funny enough, having an intuition about what caused a failure is one thing.
Proving that your opinion is objectively true is a completely different thing!
Let’s focus on what we know, and how to prove what happened!
In a typical crime-novel fashion let’s start by summarizing what we already know:
I wonder if such an arrangement of facts make it easier to see what was the cause of failure. Do you feel like you want to change your initial estimate?

All of the above, made me believe that the pressure vessel failure was a typical circumferential buckling issue.
I mean, the pictures from the inside of the shell made it pretty clear! During my work, after a few days, the removal of the failed vessels started.
This is when I also received the pictures of the internal shell from the outside:

Perhaps I just spent too much time working with shells, but the above to me looks like a “classical” case of circumferential buckling at a first glance.
For curious readers:
Those short stiffeners on the shell were only there to aid the flow of medium in the heating space.
Such short horizontal stiffeners could not help with the buckling (you would need full rings for that), and I honestly don’t think designer of the vessel treated them as helping.
In pressure vessel design circumferential buckling usually happens when there is underpressure in the vessel. This underpressure is commonly called “vacuum”, even through full vacuum is not always there:

Such vacuum/underpressure causes compression in circumferential direction of the shell, which may lead to buckling, of the kind you saw on the photos.
The problem here is, that those vessels should not have vacuum inside! The process (as designed) should not end with underpressure developed in the vessel at all!
Furthermore, the vessels that failed weren’t even in operation when failure happened!
So, we know what happened… we just don’t know how!
Luckily, we have another fact at our disposal, that will help us to identify the failure cause:
Something actually leaked during failure!
We know that the vessels that failed were not used. But we also know they were in the same installation as the small vessel that was used during the first run.
When analyzing the task, I instantly assumed, that the main chamber of the vessel was empty and “unused” during failure. After all vessel was not working during failure. I figured this is what the operator meant.
However, I suspected circumferential buckling, so I knew that something needed to cause circumferential compression in the shell. I assumed that it is at least possible that all 4 vessels have a common heating installation.
If my assumption was correct, it would solve one of the “mysteries”. It is obvious that the heating was “on” even if only one vessel was working. This would mean, that the heating space in each vessel would be full, even if only one vessel was in operation.
This fits the observations for 2 reasons:
Of course, my first question to the Customer was: do the vessels have a common heating system? And as you can suspect at this point, they confirmed my suspicions.
Learn the most valuable Nonlinear FEA lessons that will greatly speed up your learning about:
Watch the video today, and skyrocket your FEA skills!
Get the lesson here
At this point, the story is fairly straightforward I feel. But let’s get to the end!
As you can see on the sketch I’ve made, the heating space was super small (30-40mm wide if my memory serves). The amount of medium that it could contain was minimal of course. This made it easy for people to “discard this” when they explained what was happening (but also in calculations).
However, hydrostatic pressure doesn’t care how many liters of medium there is! It only cares how high the medium surface is! And in our case, with a full heating space, it would look like this:

Of course, if there would be an overpressure (due to technology) in the heating space, if would be even worse!
With this understanding, proving how the failure happened is very easy. Just use Nonlinear FEA, and you won!
Technically speaking you can make a very simple hand calculations to check that the shell “had no chance”. However, such calculations can never include those short stiffeners on the shell. And while I knew those did not help, I had to consider that someone may doubt this… so I simply included those in our model.
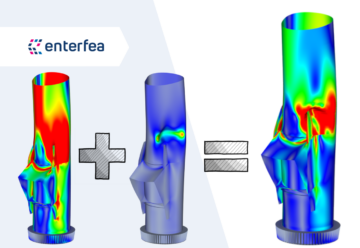
In the end, the failure of this vessel obtained in FEA looks like this:

And for failure comparison, this is the FEA outcome and the image of the pressure vessel failure (both without the outside heating jacket):

Without a doubt buckling shape is a bit random. It strongly depends on initial imperfections, and of course we could not have measured those pre-failure. But even with this in mind, the similarity of failure mode in reality and FEA is very good.
Of course, the analysis showed, that when the heating space was full (with some overpressure that was present), the inner shell had no chance! The capacity was significantly too low, and failure… simply must have happened (and it did).
From time to time my Customers ask me, why I want to analyze so many things when we do industrial calculations. To them, it may seem that some of the things are simply “unimportant” or “negligible”. It’s tempting to ignore them in design!
I usually politely reply, that we already ignored the things we believe are “unimportant”, and that the rest should really be there.
I feel this case study shows very well, why paying attention to details really matter in engineering, and why I’m so accurate when it comes to those things.
The heating space could contain about 600l of medium (0.6m3), causing a total vertical load of 6kN. This is around 6% of what the main chamber could hold.
I can easily see, how one could say this is “negligible”, especially since heating space was really narrow, so it also looked “innocent”.
Hydrostatic pressure in the heating space (along with some extra overpressure there) was a direct reason why the vessels buckled (when the main chambers were empty).
Clearly, hydrostatic pressure in the heating space was not something you could neglect in the end…
But it seemed like something that *could* be unimportant, and it actually was neglected! Not only in design, but also in testing of the vessel.
And this neglect was the direct reason that lead to vessel failure.
As I’m writing this, I’m pretty certain that the design never considered external pressure on the main vessel shell. If it would… the simplest of checks would show that something is wrong.
Sadly, I was unable to confirm if the vessel tests really happened. Personally I believe they did happen. I simply don’t want to think that someone said they did tests and simply lied.
But why the tests found no issues?
I believe, the issue lies in planning of the tests. If I would have to guess, I would say that testing order was something like this:
STEP 1: Fill in main chamber. Test for leaks and pressure in the main chamber.
STEP 2: Add medium to the heating space. With both areas filled test the heating space for leaking and pressure.
… and that’s it!
I mean, it would be deceivingly easy to think “more medium must be worse”, and “those extra 6% change nothing” during testing as well. And its very short from there to saying “let’s not waste time testing the heating space alone”.
After all, the test of the heating space with an empty main chamber would fail in any reasonable circumstances. After all, the vessels failed on the very first run of the installation!
Worth remembering:
The next time you will feel like removing something from the scope of the calculations (or someone will ask you to do so), remember that even seemingly small things may have big consequences.
Finding this fault at any stage of design, manufacturing and testing would lead to significantly less trouble and costs.
The worst thing that can happen is, that you “hope” that something is negligible, you don’t check it… and then it fails on site!
Those cases are the true nightmare of costs and legal responsibilities.
Heck, maybe even send your Customer the link to this article, so they can read about it themselves (I will do this for sure!).
In the end: If you have any interesting design, or failure you need help analyzing – definitely send me an email – I will gladly discuss it!
Above, I outlined the most important things that allowed to determine the cause of failure. However, a few more things crossed my mind when I was examining this case.
I figured you may be as curious as me, so below a few extra considerations:
I really hope that this case study shows the beauty and complexity of engineering.
Sure, this was a failed design, but thanks to the company that hired me to search for the failure, I could share the above conclusions, so we can all learn from this.
I hope you can also see that Nonlinear FEA is great at solving such issues and leaving no stone unturned. But I also hope that it’s obvious that you also need a good engineering knowledge.
After all, if you would not think to check such a load case, Nonlinear FEA wouldn’t find an issue either! You need to know what you need to check to properly use FEA (or any other design method).
I really hope you enjoyed this one!
Let me know what you think in the comments, and feel free to recommend this to any colleague of yours who may benefit from reading this case study!



Share
Join the discussion